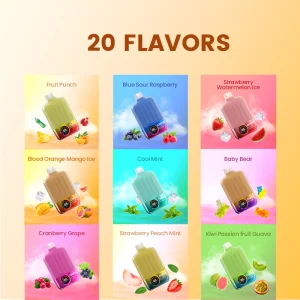
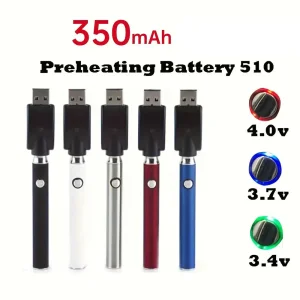
Shenzhen Nano Vape Co., Ltd. is a professional manufacturer specializing in the research, development, production, sales, and service of electronic cigarettes and electronic hookahs. With years of experience in the vaping industry, the company has established itself as a reliable partner through continuous innovation and strict quality control.
The company owns multiple patents in atomization technology and operates under internationally recognized quality management systems, including ISO9001, ISO14001, and ISO13485, ensuring efficient, standardized, and environmentally responsible production processes.
Nano Vape is committed to delivering high-quality vaping products and comprehensive solutions that meet diverse customer needs, focusing on performance, safety, and user experience.
All products have passed safety certifications from third-party testing agencies in the United States and Europe, and have obtained certifications such as CE, RoHS, and FDA. The products are exported to over 50 countries and regions, including Japan, the United States, the United Kingdom, France, and Indonesia, earning strong customer recognition worldwide.
The company strives to build a modern, innovative, and consumer-oriented vaping brand, offering cost-effective products with excellent user experience.
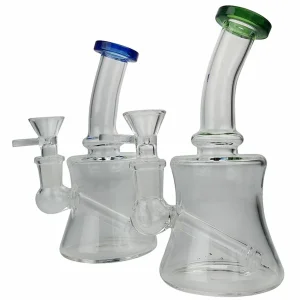
As the global shift towards smoke-free alternatives accelerates, electronic hookahs (e-shishas) have experienced exponential demand growth. Modern consumers and lounge operators demand devices that replicate traditional shisha richness without combustion toxins, driving massive OEM/ODM orders across international markets.
B2B buyers and wholesalers across Europe, North America, and the Middle East prioritize verified compliance, consistent vapor density, robust battery life, and strict child-lock safety mechanisms.
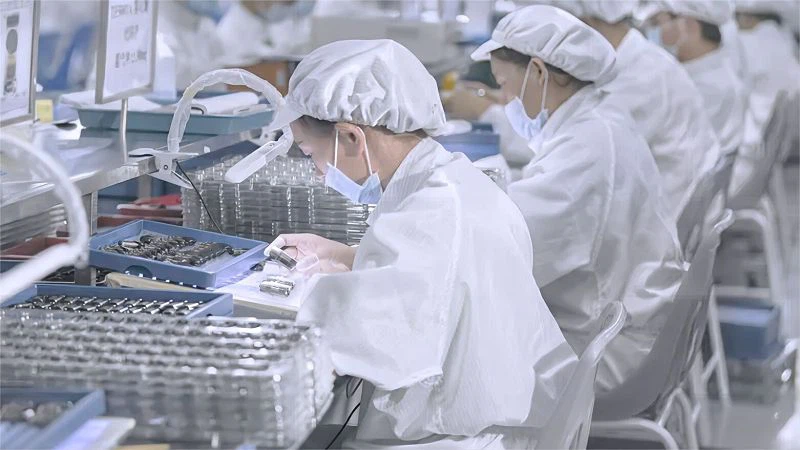
Leveraging advanced supply chain resilience, automated dust-free GMP workshops, and rigorous digital QA testing, Chinese manufacturers deliver unmatched production scalability and cost efficiency.
From high-end metropolitan vape lounges and hospitality venues to portable outdoor social gatherings, electronic hookahs offer customizable flavor profiles tailored to regional regulatory standards.
We design and develop high-performance disposable vape devices and electronic hookahs, collaborating with global clients to turn product concepts into reality through premier OEM/ODM services.
Our pod systems combine ergonomic design with advanced technology. Backed by over 10 years of industry experience, we ensure stability, safety, and consistent performance across all models.
Nano Vape prefilled pods feature advanced mesh coil technology, optimized capacity (up to 6ml), leak-proof design, and rich flavor delivery, providing a smooth and satisfying vaping experience.
We provide high-performance batteries that undergo strict quality control. Each product is rigorously tested in our in-house laboratory before commercial release.
Over 10 years of specialized expertise in e-cigarette & electronic hookah R&D, manufacturing, and global quality control.
From sales inquiry to mass production, we ensure quick communication, streamlined logistics, and reliable customer support.
Our factory operates under ISO management systems and clean GMP workshops, ensuring all products meet international CE, RoHS, and FDA safety benchmarks.
We offer full-service B2B solutions, including custom product engineering, branding consultation, technical support, and long-term partnership.
The Nano Vape team has extensive cross-disciplinary experience across the entire production chain, from precise raw material selection to final international delivery.
The R&D department works closely with the quality control team to ensure every electronic hookah and vaping device meets extraordinary standards of safety, durability, and performance. In addition, we provide customized OEM/ODM services for advanced vaping devices, including specialized solutions for nicotine salt and CBD formulations tailored to global market compliance.
Yes, all our electronic hookahs and vaping hardware undergo stringent laboratory testing and possess fully verified CE, RoHS, and FDA compliance certificates required for European and North American markets.
As a direct manufacturer with advanced factory 4.0 infrastructure, we offer flexible MOQ terms tailored to brand partners. Please contact our engineering sales team for custom branding, packaging, and flavor formulation requirements.
We operate under strict ISO9001, ISO14001, and ISO13485 management frameworks within clean GMP workshops, utilizing automated raw material inspection and multi-stage lifecycle testing to guarantee zero-defect shipments.
Our products are trusted and exported to over 50 countries globally, with primary distribution hubs across the United States, United Kingdom, Japan, France, Indonesia, and various European Union nations.
 Nano Vape